Armored Push-Pull Cable Making Machine
Produce armored push-pull cables with precision swaging and inline laser measurement.
View machineARMORED CONTROL-CABLE CORES
Wrap and swage the moving core of a control cable.
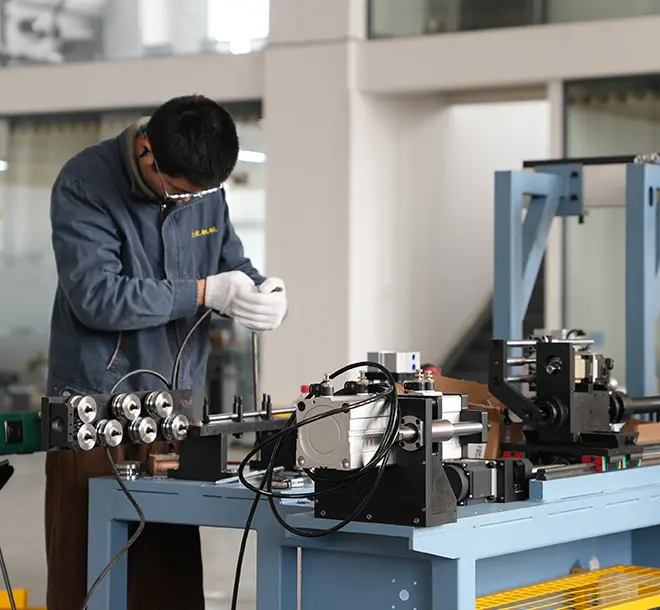
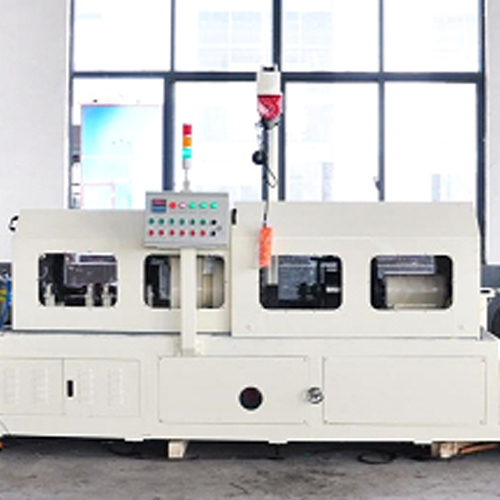
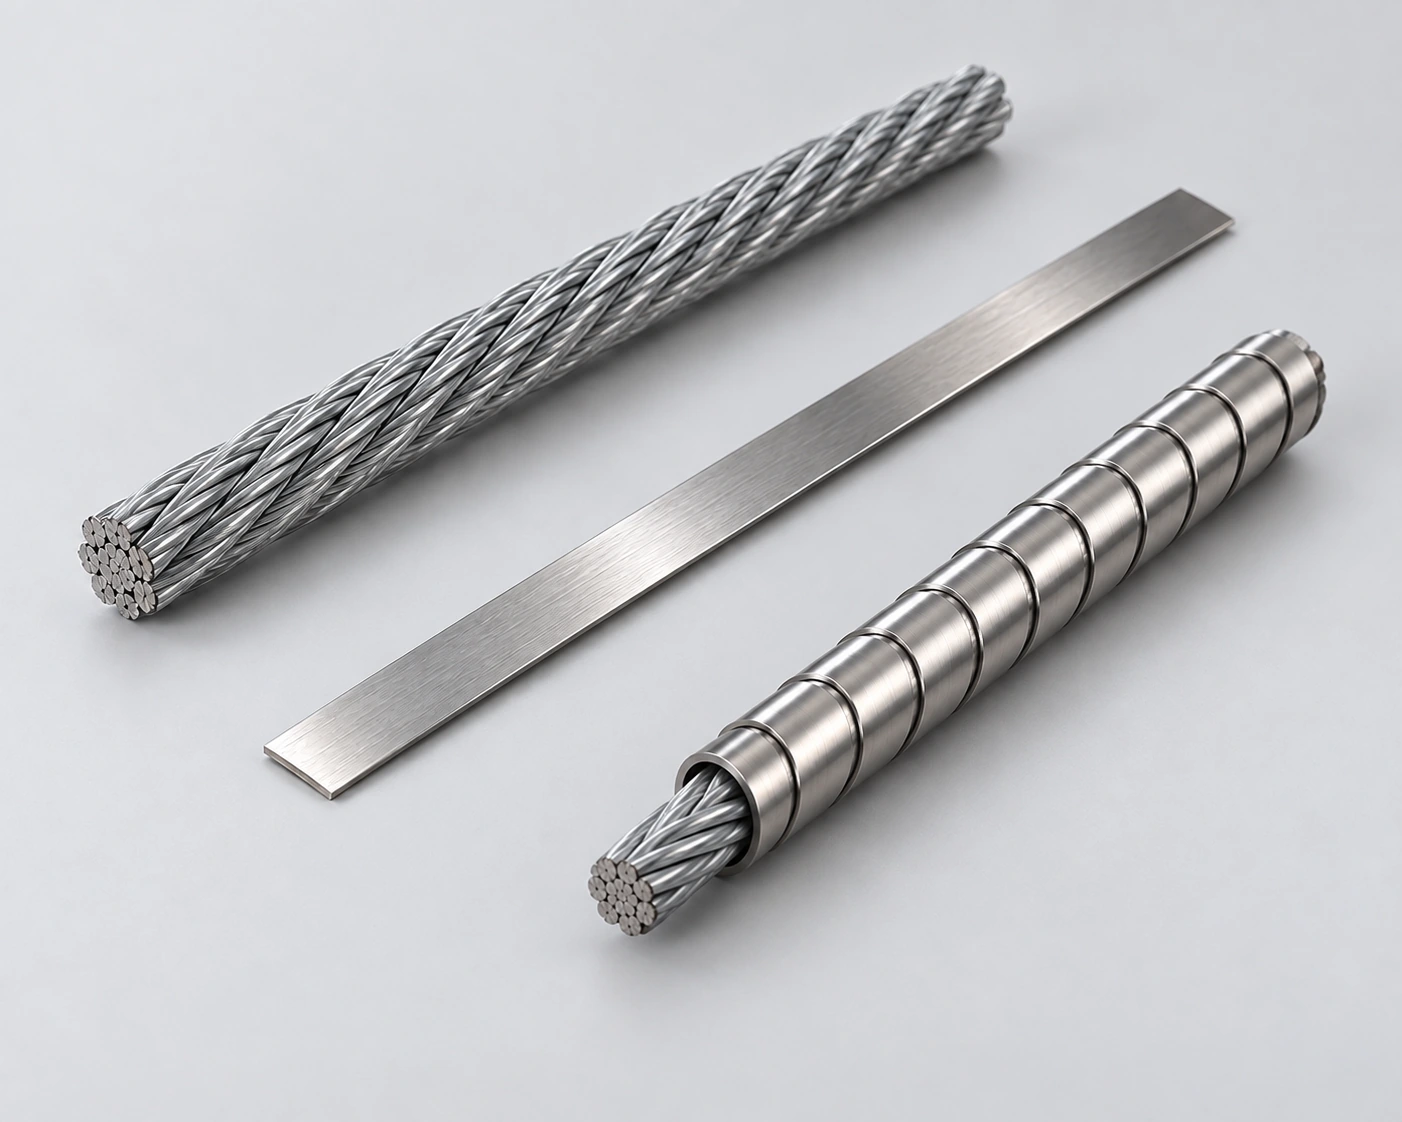
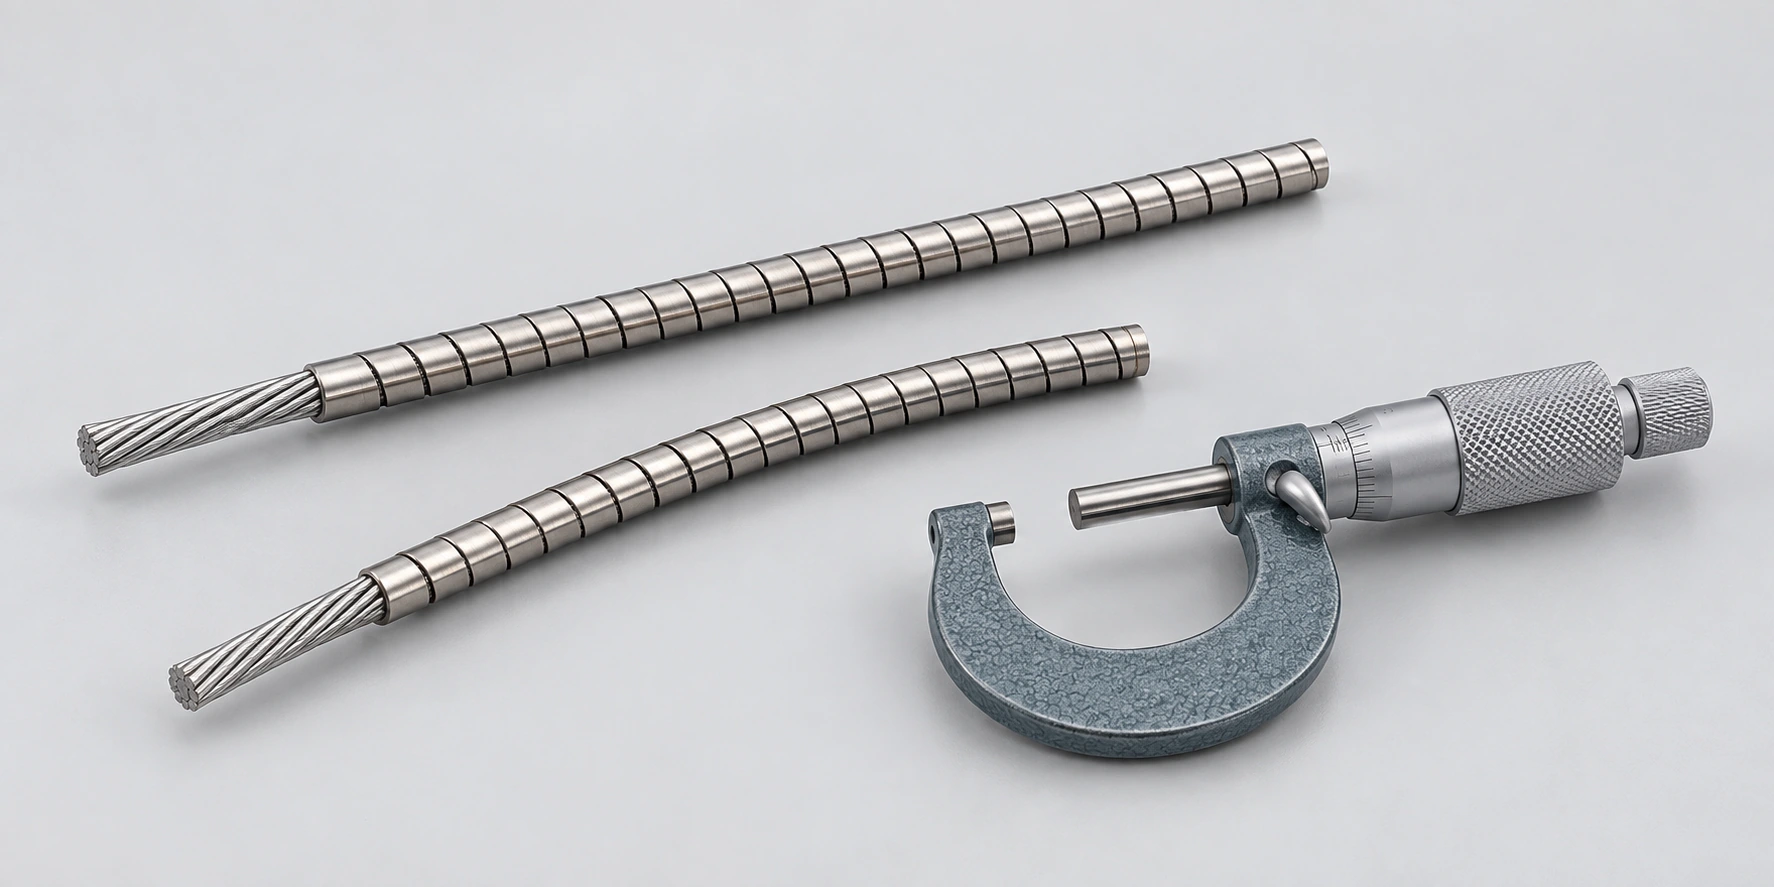
BOBO’s armored push-pull cable machine feeds wire rope, winds stainless steel strip around it and shapes the wrapped core through rotary swaging. The line combines payoff, winding, swaging and conveying, with laser outside-diameter measurement and an alarm. It serves core manufacture for clutch and gear-control cables.
Wire-rope payoff and stainless strip winding
Rotary swaging of the wrapped core
Laser diameter measurement with an alarm
Push-Pull Cable Machine
Armored push-pull core winding and rotary-swaging equipment
SPECIFY THE ARMORED CORE
Rope construction, strip section, final diameter and casing fit.
FIND YOUR MACHINE
Review the incoming rope construction, strip section and required core profile as one forming task. Adjustable feed tension and a torque-controlled pulling drive coordinate material movement through winding and swaging. Pneumatic or liquid cleaning is an optional addition, to be specified for the intended process.
Produce armored push-pull cables with precision swaging and inline laser measurement.
View machineWorking ranges are model-specific. Confirm material, product dimensions and the required operation against the selected machine.
PARTS & APPLICATIONS
The wrapped core is the moving member inside a separate control-cable casing. Its outside profile and fit within the selected liner are part of the assembly design; making the core does not complete the casing, end fittings or functional checks.
01
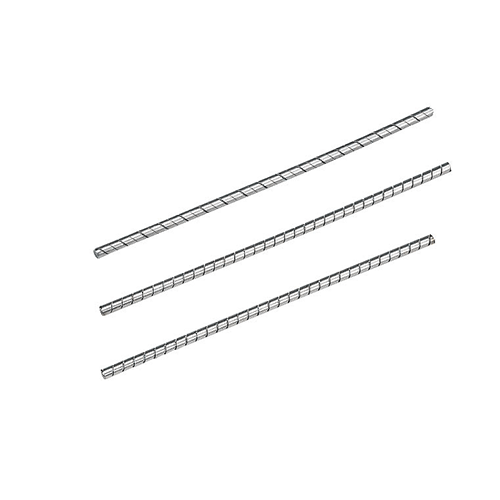
These wrapped-core examples show the outer helical strip used on the moving member of a push-pull cable. BOBO’s winding and swaging route serves clutch and gear-control cores; the mating casing and end connections are specified separately.
SELECTION GUIDE
Select the forming setup around the rope diameter and construction, stainless strip dimensions and target diameter after swaging. Include the casing clearance and routing conditions in the component specification so the trial assesses a usable core, rather than diameter alone.
01
Review the wire-rope construction and diameter together with stainless strip grade, width and thickness. Include reel dimensions and the feed condition required at the winding station.
02
Specify the strip arrangement, diameter after swaging and surface condition. Match the winding and swaging tooling with the tension and pulling setup, then agree dimensional checks on trial lengths.
03
Identify collection, cutting or further processing after core forming. Assess the trial core in its intended casing, with the route, travel and loading conditions used for the final cable’s acceptance.
Push and pull load, travel, friction and durability belong to the assembled control cable. Specify those checks separately from line speed and the core’s outside-diameter measurement.
YOUR FINISHED PART
Include the material, dimensions and acceptance requirements.
From technical review and testing to delivery and after-sales.
BOBO can review rope and strip samples with the finished-core drawing to define winding, swaging and feed settings. Agree inspection of the wrapped profile and diameter, then identify the fit and movement checks needed in the intended casing. Include swaging lubrication, any optional cleaning, operator training and service tooling in the supply discussion.
Rope, strip and finished-core review
Winding, swaging and feed-setting trials
Diameter, surface and mating-fit checks
Lubrication, cleaning options and operator preparation
BEFORE YOU CHOOSE
Distinguish the manufactured core from the complete control-cable assembly.
No. It winds stainless strip around wire rope and rotary-swages that wrapped member to make an armored inner core. The outer casing, liner and end fittings are separate parts of the final control cable.
Here the swaging unit shapes the wrapped core as it passes through the line. Attaching a terminal or end fitting is a separate operation with its own component and tooling requirements. Do not use a core-forming specification as an end-connection specification.
The laser system monitors outside diameter and raises an alarm. Set the acceptance limits for core diameter and specify separate tests for push load, pull strength, friction and service life. Diameter monitoring is not a substitute for those assembly checks.
Pneumatic or liquid cleaning is optional. The rotary swaging unit has an automatic oil-lubrication system, which serves the forming equipment. Select any cleaning arrangement around the surface condition required for the next operation.
START WITH A DRAWING OR SAMPLE
Include rope material and construction, incoming diameter, strip grade, width and thickness, target core diameter and tolerance, and the required surface condition. Add reel sizes, target production rate and the next cutting or assembly step.
Include the mating casing or liner dimensions and the control cable’s route, travel and load requirements so the trial and final assembly checks address its intended use.
Push-Pull Cable Machine / BOBO MACHINE