Mandrel vs Mandrel-less Tube Bending: Choosing the Right Method for Your Application
Jump to section
Tube bending fails when manufacturers pick the wrong internal support method. Mandrel bending uses a solid rod inside the tube to stop it from collapsing during tight bends. Mandrel-less bending skips that rod and works best on thicker tubes with larger bend radii. The right choice affects part quality, cost, and whether a bend meets spec.
The decision comes down to wall thickness, bend radius, and material. A thin-walled tube needs a mandrel for a tight bend. Without one, it will wrinkle or collapse. The same tube bent to a gentle curve may not need one at all.
This guide compares both methods, explains which tube parameters call for mandrel support, and covers when each method fits a given production run.
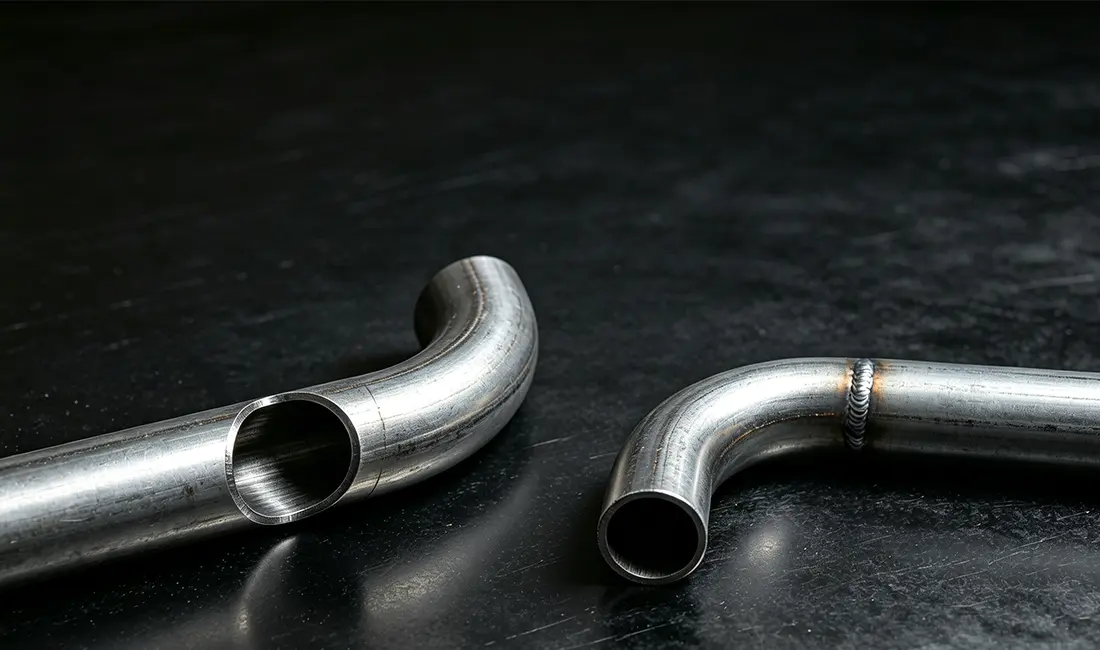
The main difference is internal support. Mandrel bending uses a solid rod inside the tube to prevent collapse. Mandrel-less bending has no internal support and relies on the tube’s own strength.
Mandrel tube bending inserts a solid metal rod inside the tube during the bend. This rod supports the inner wall and stops the tube from collapsing or wrinkling.
The mandrel stays in place as the tube bends around a die. It pushes back against the compression forces on the inside of the bend. This keeps the tube round and keeps the wall thickness even.
Manufacturers use this method for tight-radius bends and thin-walled tubes. It works best when the diameter-to-wall-thickness ratio is above 25:1. These thin tubes cannot hold their shape on their own.
Mandrel-less tube bending bends the tube around a die with no internal support. The tube relies on its own wall strength to hold its shape.
This method suits tubes with thick walls and large bend radii. It also costs less and sets up faster, since there is no mandrel to insert or remove.
On tight bends, though, the inner wall can flatten and the wall thickness can turn uneven. This limits mandrel-less bending to jobs where minor deformation is acceptable.
Mandrel bending keeps tube shape steady but costs more to set up. Mandrel-less bending sets up fast and costs less, but risks deforming the tube. The right choice depends on bend radius, wall thickness, and production volume.
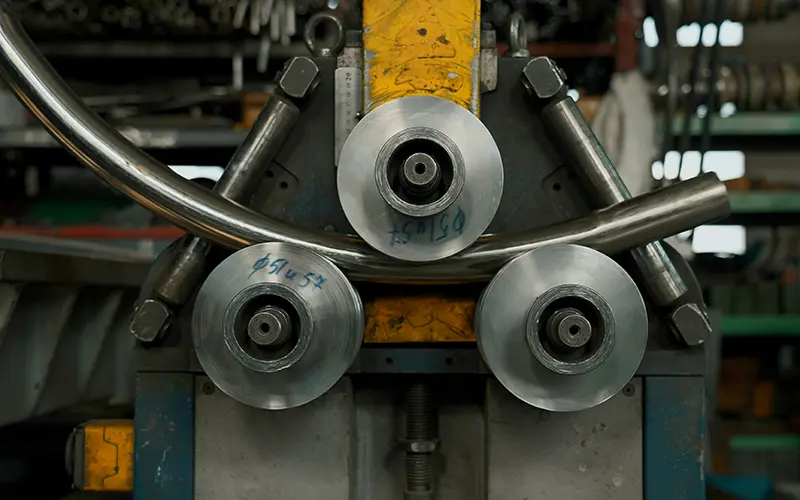
A mandrel supports the tube from the inside, which keeps wall thickness even and produces smooth, wrinkle-free bends.
Advantages:
Disadvantages:
Mandrel-less bending shapes the tube around a die with no internal support, relying on the tube’s own wall strength.
Advantages:
Disadvantages:
| Factor | Mandrel Bending | Mandrel-less Bending |
| Minimum Bend Radius | 1.5× tube diameter | 4× tube diameter |
| Setup Cost | 5,000−5,000-5,000−15,000 per mandrel | 500−500-500−2,000 per die |
| Setup Time | 30-60 minutes | 10-15 minutes |
| Wall Thickness Range | 0.020-0.250 inches | 0.065-0.500 inches |
| Scrap Rate | 2-5% | 8-15% |
Mandrel bending suits high-volume runs where bend quality is worth the setup cost. Mandrel-less bending suits prototypes or gentle bends where deformation risk is low. Tubes under 0.065 inches wall thickness need a mandrel to avoid collapse.
Wall thickness, bend radius, and material determine whether a tube needs a mandrel. Thin tubes bent to a tight radius need one. Thick tubes bent to a gentle radius often don’t.
Two numbers drive this decision. The first is the wall factor. This is the tube’s outer diameter divided by its wall thickness. Some shops call it the D/t ratio.
The second number is the D of bend. This is the centerline radius divided by the outer diameter. This guide calls the same number “3D” or “4D” elsewhere.
These two numbers work together. A wall factor below 15 and a D of bend above 6 usually need no mandrel at all. A wall factor above 25 always needs one, even on a gentle bend. Between those points, check the actual bend radius before you skip the mandrel.
Stainless steel, titanium, copper-nickel, and T6 aluminum wrinkle more easily than mild steel. These materials need firmer mandrel support. High-nickel stainless steel (314, 329) and nickel alloys like Inconel can deform more before they collapse. These materials need less aggressive mandrel setups.
Surface quality matters too. Rough tube surfaces create more friction against the tooling, which can cause marking or distortion. Smooth, clean tubes bend more predictably and can use a slightly looser mandrel fit.
Yes. Wrinkles form in two common cases. The mandrel may sit too far back from the tangent point. Or the nose diameter may be too small. Either error lets the tube’s inner wall buckle before the mandrel can support it.
Common setup errors that cause wrinkling:
Bend angles beyond 180 degrees raise the risk too. The tube spends more time under stress, which can overwhelm the mandrel’s support.
The choice depends on wall thickness, bend radius, and the finish quality a part needs. Matching these three factors to the right method up front saves rework and scrap later.
Mandrel bending fits thin tubes and tight bends. Below 3 times the tube diameter (3D), the risk of wrinkling rises fast without internal support.
Applications requiring mandrel bending:
This method fits tubes under 0.065 inches wall thickness. Stainless steel needs it more often than other materials, since it wrinkles easily.
Mandrel-less bending fits thick tubes and gentle bends. Tubes over 0.125 inches wall thickness usually resist collapse on their own, especially above 4 times the tube diameter (4D).
Applications using mandrel-less bending:
This method also fits prototypes and small batches, since setup takes minutes instead of hours. Minor cosmetic deformation is often acceptable in these jobs.
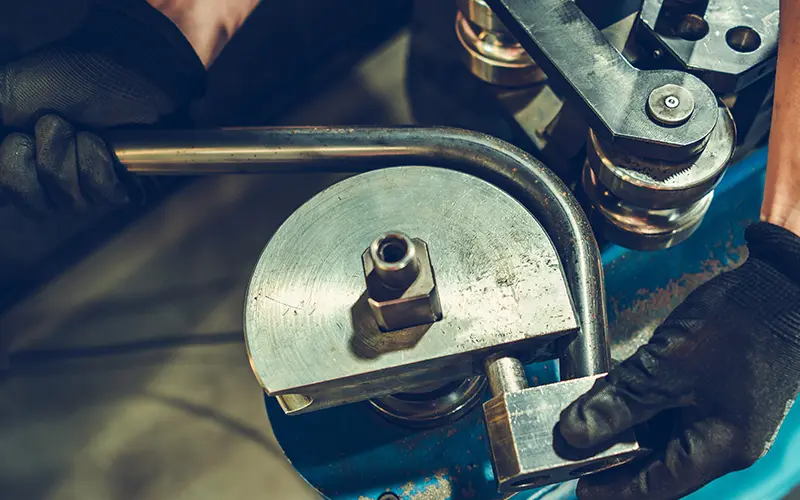
Wall thickness, bend radius, and part tolerance all affect this decision.
The D/t ratio (outer diameter divided by wall thickness) is a fast way to check. A ratio above 25 usually needs a mandrel. A ratio below 15 usually doesn’t. Ratios in between call for a closer look at the actual bend radius.
Key factors for method selection:
| Factor | Mandrel Needed | Mandrel-less OK |
| Bend radius | Under 3D | Above 4D |
| Wall thickness | Under 0.065″ | Above 0.125″ |
| D/t ratio | Above 25 | Below 15 |
| Surface finish | Critical | Flexible |
Production volume matters too. Mandrel setups cost more upfront but cut scrap in long runs. Parts that need ±0.5 degrees of angular accuracy also need mandrel support. This keeps the tolerance steady.
BOBO’s mandrel tube bender supports the tube wall through the full bend cycle. This keeps wall thickness steady on tight-radius work like exhaust systems and roll cages. For thicker tubes and gentler bends, BOBO’s CNC tube bending machine handles mandrel-less setups on the same production line, which cuts changeover time between tube sizes.
A tube without enough support tends to fail one of two ways. Thin tubes usually collapse or flatten along the inside of the bend. Tubes with more wall thickness tend to wrinkle instead, buckling in small ripples on the inner radius. Either sign points to the same fix: add mandrel support, or open up the bend radius.
Mandrel tube benders typically handle tubes from 0.25 to 6 inches in diameter. Wall thickness usually ranges from 0.020 to 0.250 inches. Tubes under 0.065 inches usually need a mandrel to avoid collapse. Tubes over 0.125 inches often don’t, since the wall alone can resist deformation. A D/t ratio above 25:1 is a reliable sign that a mandrel is needed.
Bends tighter than 3D need mandrel support. The inside of the bend faces more stress at this radius. Bends looser than 4D can often skip the mandrel. This works as long as the wall is thick enough on its own.
Soft materials like aluminum and copper collapse easily, so they usually need a mandrel. Harder materials like stainless steel and titanium resist deformation better, but tight bends in these materials still need one.
The choice between mandrel and mandrel-less bending comes down to wall thickness, bend radius, and material. Thin walls, tight bends under 3D, and materials prone to wrinkling call for a mandrel. Thick walls, gentle bends above 4D, and forgiving tolerances make mandrel-less bending the faster, cheaper option. BOBO Machine builds both mandrel tube benders and mandrel-less setups. These fit production lines that switch between tight and gentle bends. Contact BOBO Machine to match the right method to a specific tube spec.